logo

products details

Created with Pixso. Home Created with Pixso. Products Created with Pixso.
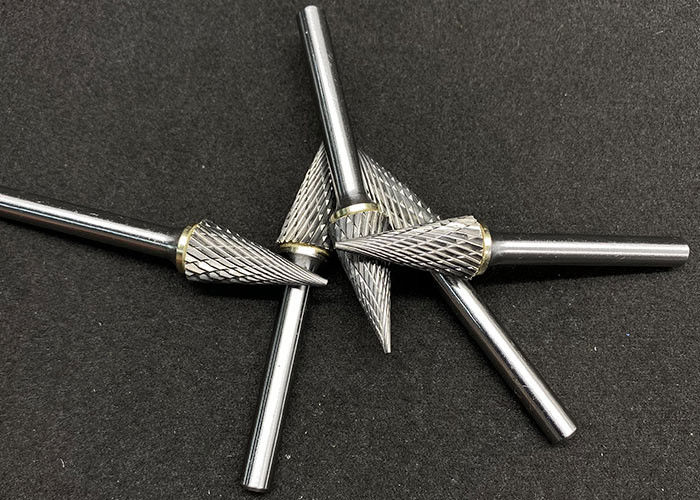
Cone Carbide Burr
Created with Pixso.

Metal Grinding Polishing High Speed Carving Burrs Impact Toughness

Metal Grinding Polishing High Speed Carving Burrs Impact Toughness

Brand Name: KTS
Model Number: Custom
MOQ: 100 Pieces
Price: $1-$10/Piece
Payment Terms: T/T,Western Union
Supply Ability: 250000 Piece/Pieces per Month
Detail Information
Place of Origin:
Sichuan, China
Certification:
ISO9001:2008
Material:
Tungsten Carbide
Shank Material:
40 CrMo
Grade:
YG6/YG8/YG10X
Cut Type:
Cross, Spiral, Aluminum
Max Sink Depth:
1/3 Of Periphery
Chip Shape:
Powdery, Needle-like
Packaging Details:
Plastic Case
Highlight:

carbide carving burrs

,

high speed carving burrs

Product Description
Cutting Styles & Performance Characteristics
Cross Cutting

The most widely used shape. Offers lower cutting resistance than spiral cuts. Produces powdery chips and is capable of minimizing chattering during operation.

Spiral Cutting

A large cutting depth helps to shorten the required time for cutting. Produces needle-like chips. Somewhat higher in cutting resistance than a master cut, but capable of fast cutting. Hence, suitable for high-efficiency cutting processes.

Aluminum Cutting

Chip pocket widened to prevent clogging, enhance work performance, and help smooth chip discharge.

Recommendations for Use
  • It may be necessary to alter the running speeds from those shown in the speed chart in order to achieve optimum performance.
  • Harder materials require slower running speeds.
  • Smaller burrs require faster running speeds.
  • Long shank burrs require slower speeds for safety reasons.
  • Apply constant movement and light pressure when using the burr.
  • Running below the optimum speed will cause chipping.
  • Running above optimum speed will cause premature tooth wear.
  • Allowing the burr to become too hot may cause the braze to soften, and cause the head to become detached from the shank.
  • Using tools and collets which have become worn will encourage chipping.
  • Do not sink the burr for more than one third of its periphery.

Note: Always observe recommended operating parameters to ensure safe and efficient performance.