logo

products details

Created with Pixso. Home Created with Pixso. Products Created with Pixso.
Cone Carbide Burr
Created with Pixso.

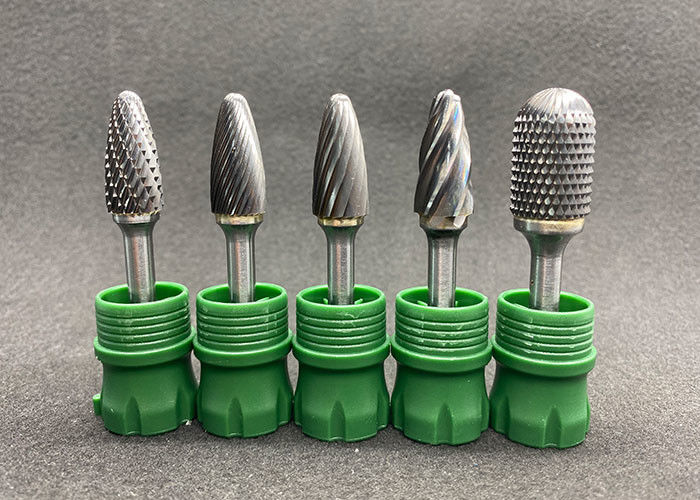
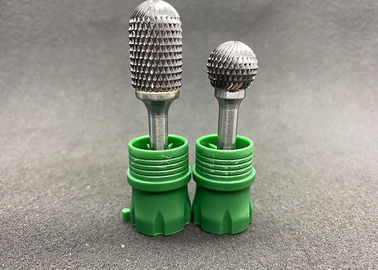
High Hardness Cone Carbide Burr Long Shank Die Grinder Bits OEM Service

High Hardness Cone Carbide Burr Long Shank Die Grinder Bits OEM Service

Brand Name: KTS
Model Number: Customized
MOQ: 100 Pieces
Price: $1-$10/Piece
Payment Terms: T/T,Western Union
Supply Ability: 250000 Piece/Pieces per Month
Detail Information
Place of Origin:
Sichuan, China
Certification:
ISO9001:2008
Material:
Tungsten Carbide
Grade:
K20/K30
Size Range:
3-25mm
Cut Type:
Single Cut/Double Cut/Diamond Cut
Burr Size:
2.4mm, 3.0mm, 6.0mm, 13.0mm, 16mm
RPM Range:
7,650-26,000
Packaging Details:
Plastic Case
Highlight:

carbide carving burrs

,

high speed carving burrs

Product Description
High Hardness Cone Carbide Burr Long Shank Die Grinder Bits — OEM Service

Tungsten carbide burrs are precision rotary cutting tools designed for deburring, shaping, and stock removal across a wide range of metals and materials. Our high hardness cone carbide burrs with long shanks deliver consistent cutting performance and are available with full OEM customization to meet your specific application requirements.

Size Selection

Tungsten carbide burrs come in a variety of sizes to suit different applications. Choosing the right size depends on the job at hand. Generally, smaller burrs are used on smaller applications for producing finer, smoother work. Larger burrs are for higher, faster stock removal and are more often used on larger jobs.

Size No. Burr Size RPM
No.42 2.4 mm 17,000–26,000
No.43 3.0 mm 17,000–26,000
No.1 6.0 mm 11,000–16,500
No.5 13.0 mm 8,000–12,000
No.6 16 mm 7,650–11,500
Speed Guidelines

The rotary tool speed you use will depend on the metal and the size and type of burr used. For optimum performance and results, it is always best to check the manufacturer recommendations for the correct RPM to use with each metal burr. Ideally, you will start off at a lower speed and increase as you go along; however, if you find your burr is chipping, it is a sign you are going too slow. Refer to the RPM ranges in the size table above as a general rotary tool speed guide.

Technique for Best Results

For the best results, and to make your burr last longer, make sure you do not use too much pressure while cutting. Too much pressure will cause the cutting edges of the flutes to chip and become smooth prematurely, reducing the life of your burr.

You will also want to ensure you keep the burr moving around the cutting area as much as possible. If the metal burr is left still for too long, this can cause clogging and stop it from digging and jabbing into the job, leaving a rough finish with visible marks.

Tip: Maintain light, consistent pressure and keep the burr in motion for a smoother finish and extended tool life.